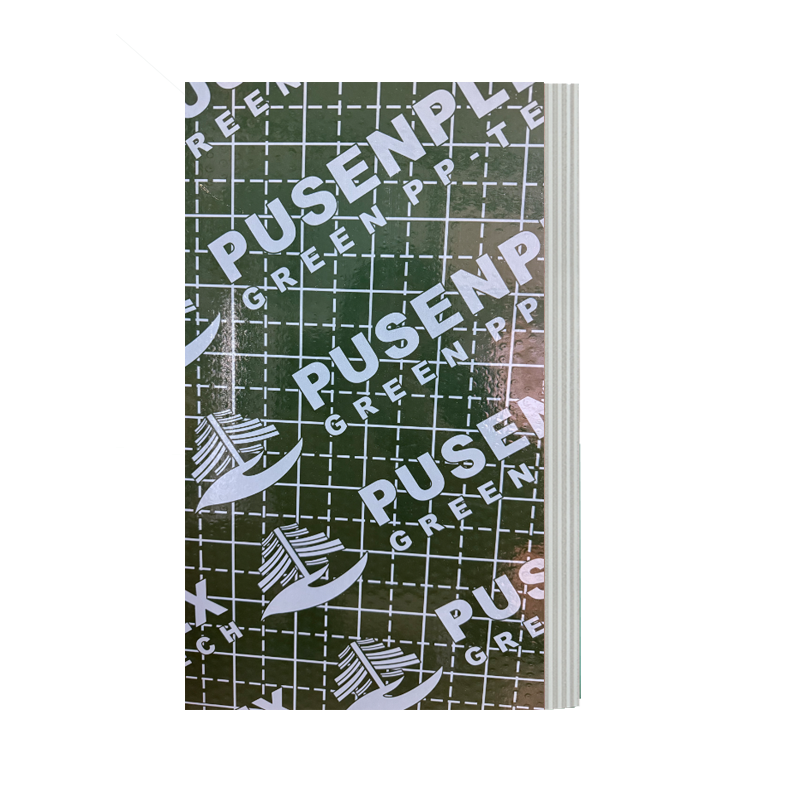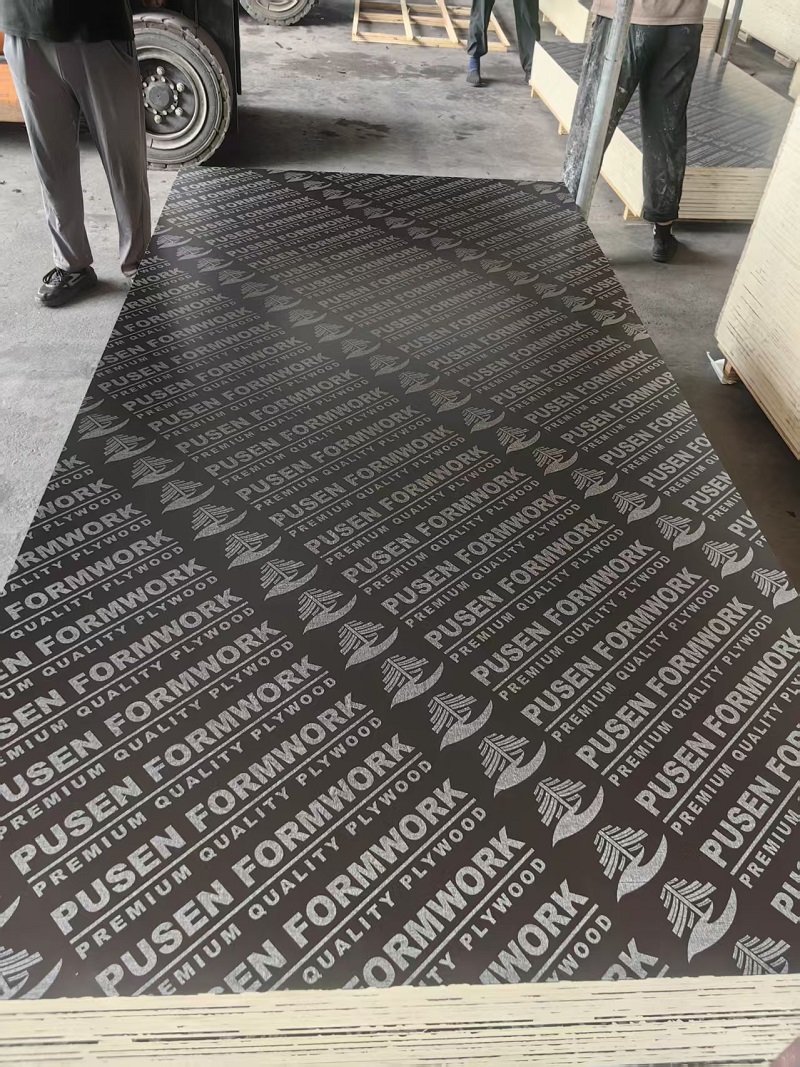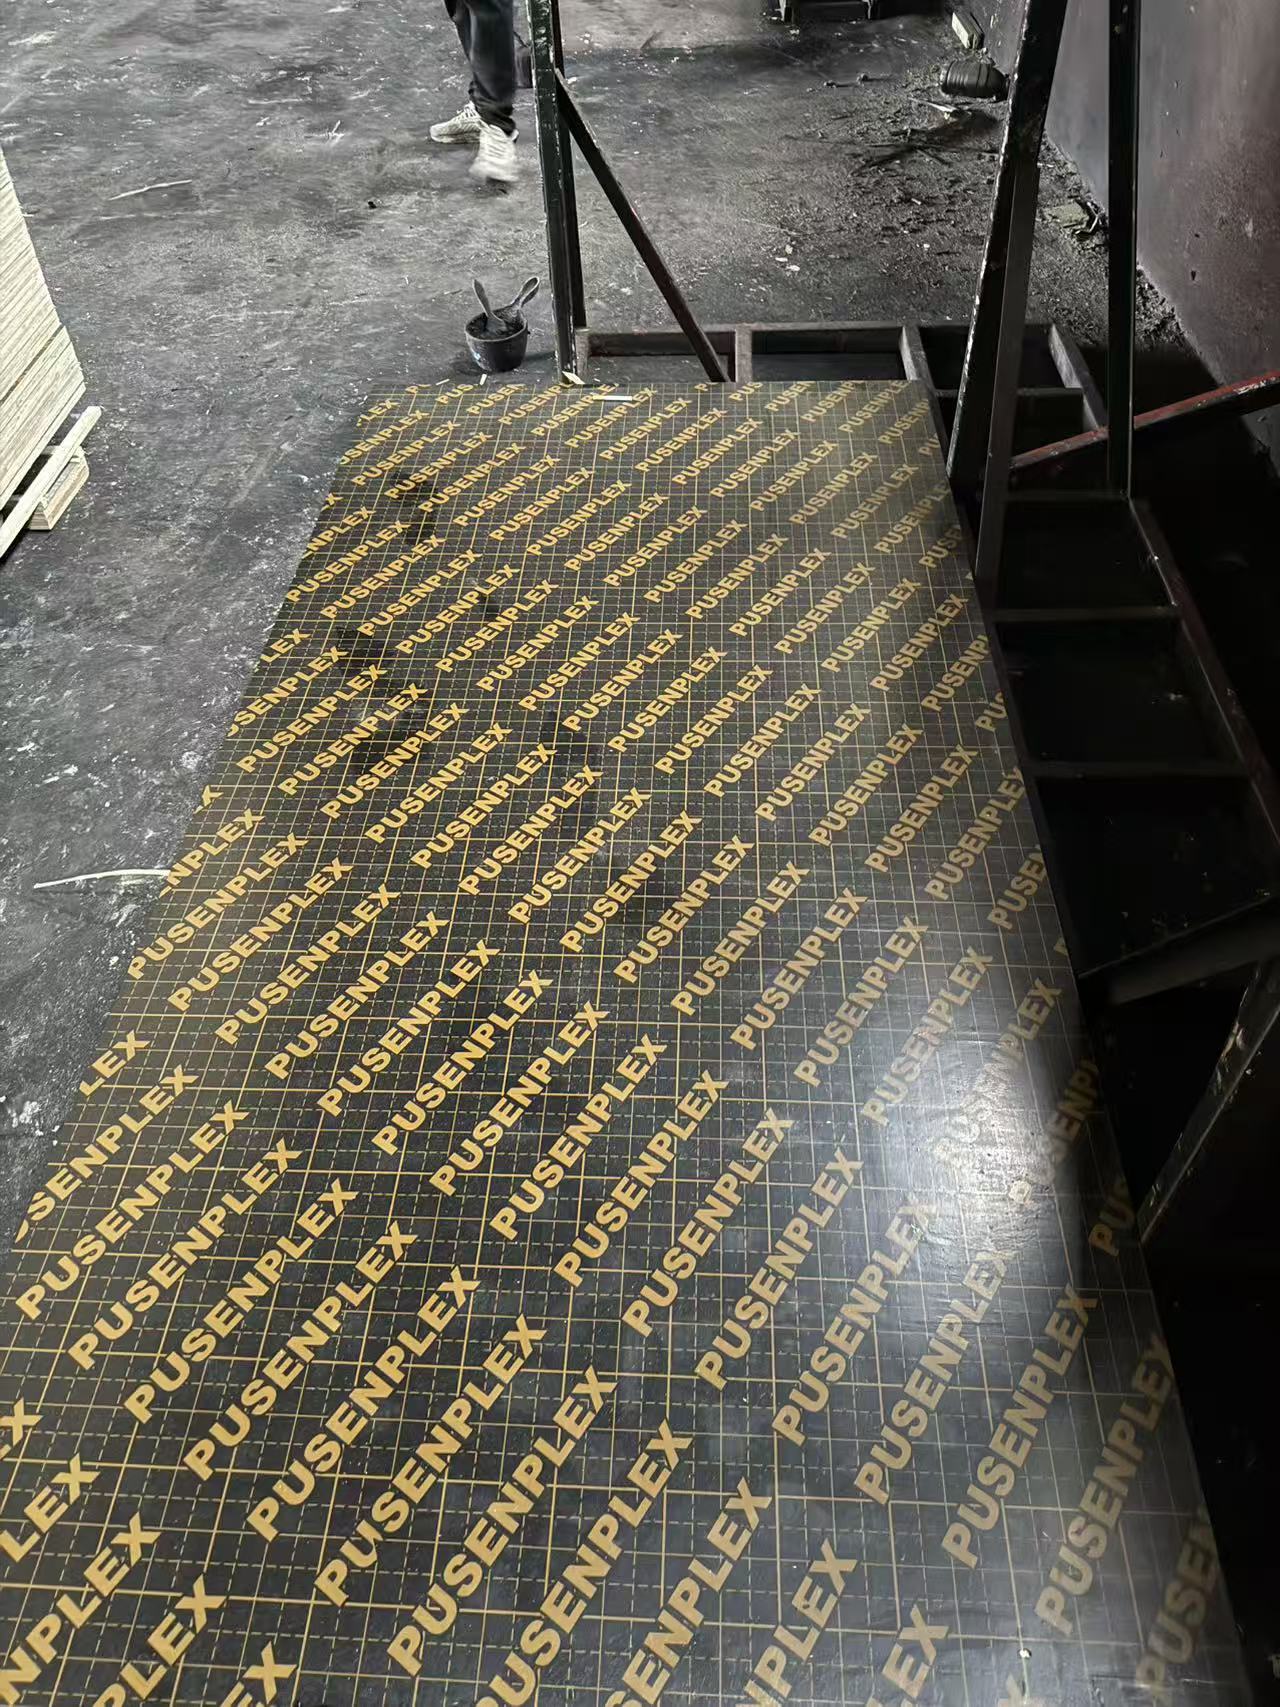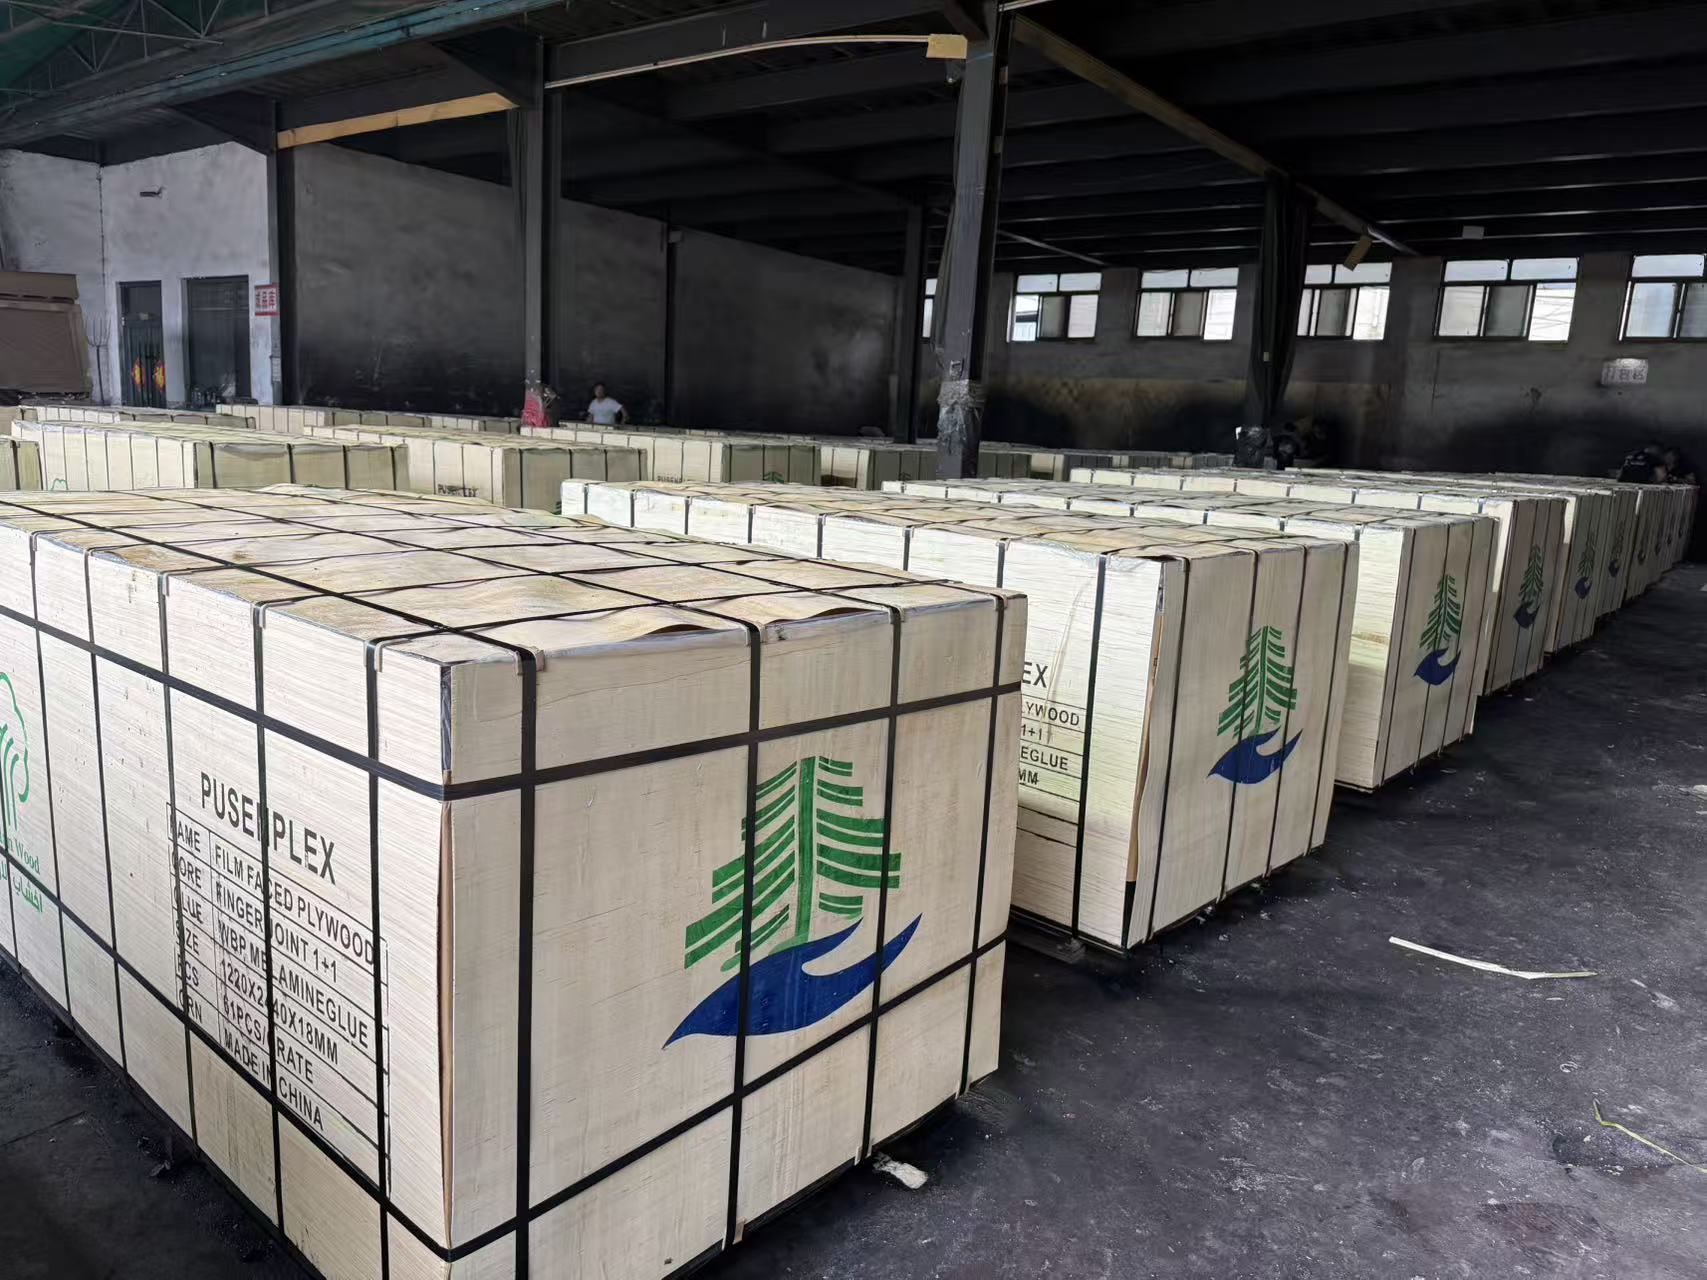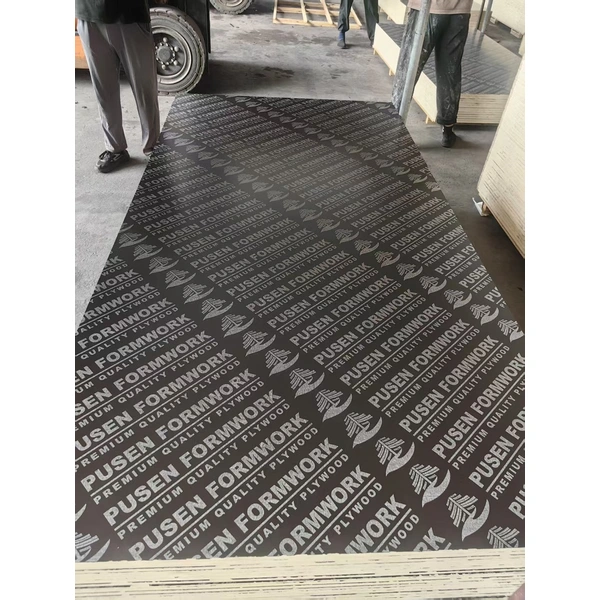
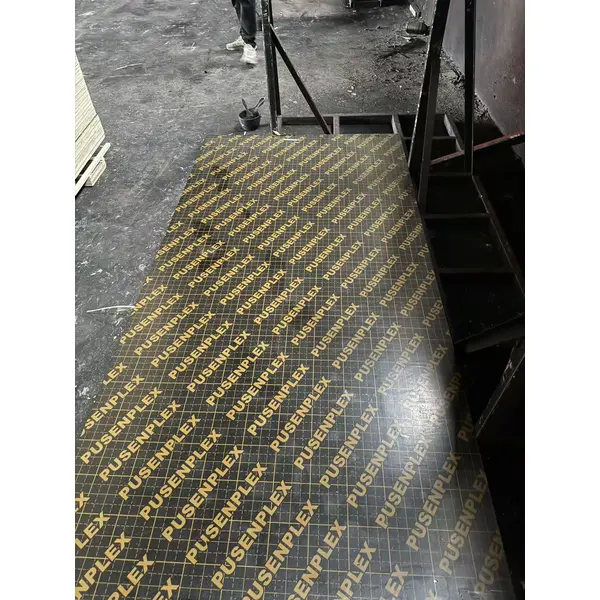
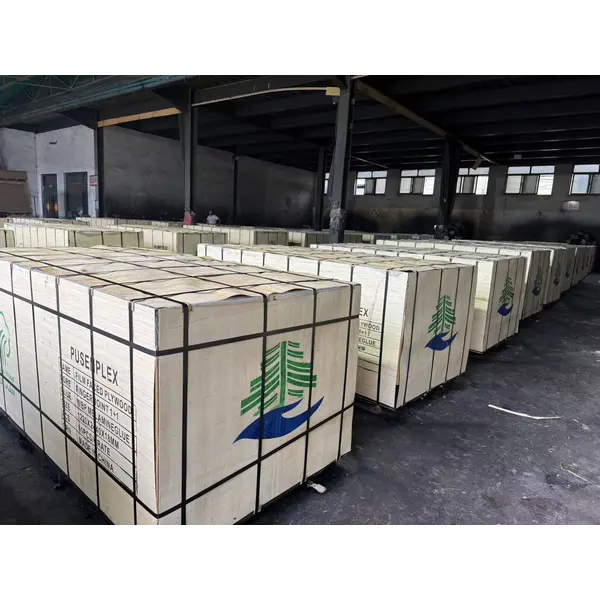

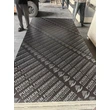


According to the repeated using times,PUSENPLEX film faced plywood have below differently quality:
PUSEPLEX-HARDWOOD(☆☆☆☆☆)
Dynea film,Phenolic glue,full hardwood core(eucalyptus),can be used 15-20 times
PUSEPLEX-COMBI(☆☆☆☆)
Brown film,WBP melamine glue,combi core(eucalyptus+poplar),can be used 8-12 times
PUSEPLEX-POPLAR(☆☆☆)
Brown film,WBP melamine glue,poplar core,can be used 6-10 times
PUSEPLEX-RECYCLE(☆☆)
Black film,WBP melamine glue,recycle core,can be used 1-4times
Why customers choose PUSENPLEX ?
We provide premium quality, eco-friendly plywood sourced from sustainable wood. Our Film Faced Plywood ensures professional results, long service life, and excellent cost efficiency for contractors, builders, and manufacturers worldwide.
What options you can choose from PUSEN WOOD ?
No.1: you can choose differently film
Dynea film paper-160-200g/㎡ Dynea is a well-known brand of impregnated paper in Finland, which is widely used in shuttering plywood production.
Phenolic film paper-160-200g/㎡ Excellent resistance to water, weather, chemicals and high temperatures, suitable for high-end construction formwork.
Melamine film paper-120-140 g/m² Waterproof performance is better than MR glue, but not as good as phenolic resin glue, suitable for some mid-range building formwork.
MR/UF film paper-100-120 g/m² weakly waterproof, used for some simple packaging or non-load-bearing temporary structures.
No.2: you can choose differently glue:
WBP phenolic glue: 72 hours in boliling water
WBP melamine glue:24-48 hours in boliling water
Melamine glue:12-24 hours in boliling water
No.3: you can choose differently core:
Hardwood/combi/poplar/recycle
No.3: you can choose differently pressing
One time hot press one time cold press
Two tmes hot press one time cold press
Film Faced Plywood – Quality FAQ
Delamination (Layer Separation)
Problem: Layers may separate under moisture or stress.
Cause: Poor adhesive, uneven pressing, or wet storage.
Our Solution:
Use premium phenolic resin adhesives
Control pressing temperature, pressure, and time
Store plywood in dry, ventilated conditions
Surface Blisters or Bubbles
Problem: Small bubbles or blisters on the film surface.
Cause: Trapped moisture, uneven heat/pressure, or low-quality film.
Our Solution:
Pre-dry veneers before lamination
Maintain uniform pressing conditions
Store film in dry, flat conditions
Film Peeling at Edges
Problem: Film lifting or peeling from plywood edges.
Cause: Insufficient adhesion, poor edge sealing, or rough handling.
Our Solution:
Ensure full adhesion with proper pressing
Seal edges carefully
Handle plywood gently during transport
Warping or Bending
Problem: Plywood may twist, bend, or warp.
Cause: Uneven moisture, poor stacking, or sudden humidity changes.
Our Solution:
Maintain consistent veneer moisture
Store panels flat in ventilated areas
Stack and transport properly
Cracks or Splits
Problem: Plywood may crack under stress or temperature changes.
Cause: Defective veneers, mechanical stress, rapid environmental change.
Our Solution:
Use high-quality, defect-free veneers
Handle carefully and acclimate to conditions before shipment
Uneven Gloss or Color
Problem: Surface may appear uneven in color or shine.
Cause: Inconsistent heat/pressure, film thickness variations, or premature UV exposure.
Our Solution:
Apply uniform pressing and curing
Use premium, consistent film materials
Our Film Faced Plywood is produced under strict quality control, with each step carefully monitored to guarantee superior durability, smooth finish, and reliable performance for construction and industrial projects worldwide.